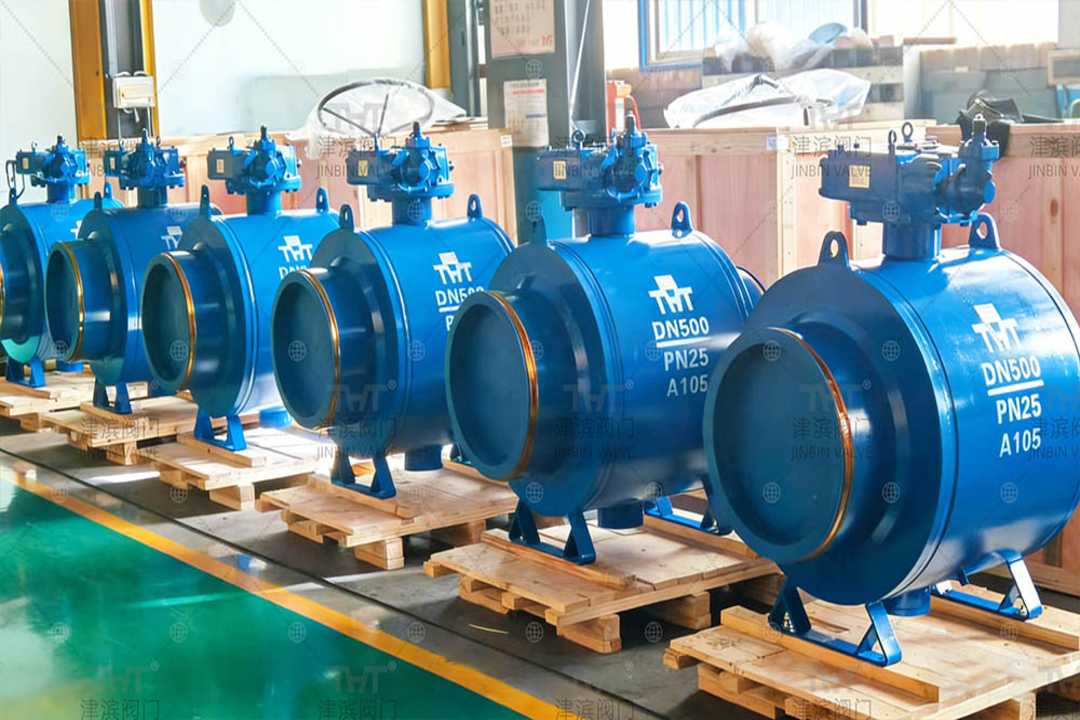
Jinbin Valve has completed the production and shipment of a new batch of large-diameter welded ball valves destined for Belarus. The valves, ranging from DN250 to DN500, were manufactured in strict accordance with customer specifications and underwent multiple rounds of workshop inspection and quality testing prior to dispatch. All units have now been safely transported to meet project delivery schedules.
Each fully welded ball valve features a blue anti-corrosion coating designed to resist both soil and atmospheric corrosion, ensuring reliable performance in demanding environments. A worm gear transmission system is installed on the valve top, enabling smooth and efficient manual operation. The design also allows for reserved interfaces for electric or pneumatic actuators, making remote and automated control possible when required.
For ease of maintenance, the valve body includes a drain and vent connection at the bottom, simplifying pipeline emptying and servicing. The valves are engineered with a compact structure and balanced weight distribution, allowing convenient installation and lifting on site. Their durable construction makes them well suited for long-distance pipeline systems and other critical applications where reliability is essential.
Full-bore welded ball valves are widely used across several sectors. In urban gas transmission and distribution networks, they support safe and stable gas delivery in trunk pipelines, gate stations, and pressure-regulating facilities. In long-distance oil transportation systems, they serve as shut-off valves for crude and refined oil pipelines, providing emergency isolation and sectional control.
They are also suitable for district heating networks handling high-temperature hot water or steam, where resistance to temperature and pressure changes is vital. Additional applications include chemical processing and refining, where pipelines may carry corrosive, flammable, or hazardous media, as well as municipal water supply and drainage systems, where large-diameter control valves are required in water treatment or sewage facilities.
Jinbin Valve specializes in project-based valve solutions and custom-designed products tailored to customer requirements. The company’s engineering team works closely with clients to select appropriate designs that balance performance, reliability, and cost efficiency.