John Crane, a global specialist in flow-control technologies and a business of Smiths Group plc, has successfully completed a major sealing retrofit at a leading copper mining operation, delivering substantial reductions in water consumption while improving maintenance efficiency on a critical slurry-handling asset. The project involved the installation of a mechanical seal package on a large underflow thickener slurry pump used within the mine’s tailings management system. The retrofit is expected to reduce clean water consumption for sealing purposes by approximately 288,000 litres per day, while also helping the operation minimise maintenance-related downtime and safety exposure.
Underflow thickener pumps play a vital role in transporting high-density slurry from thickening systems into tailings transport circuits. In this application, the Warman 550 pump operates with slurry concentrations of approximately 65% solids, making reliability essential to uninterrupted mining operations.
Before the upgrade, the pump relied on a conventional stuffing box packing arrangement. The abrasive nature of the application caused significant wear on the shaft sleeve, requiring replacement every four months. These maintenance interventions were resource-intensive, involving a full mechanical crew working across two shifts, approximately 36 hours of maintenance activity, and the deployment of a 100-tonne crane.
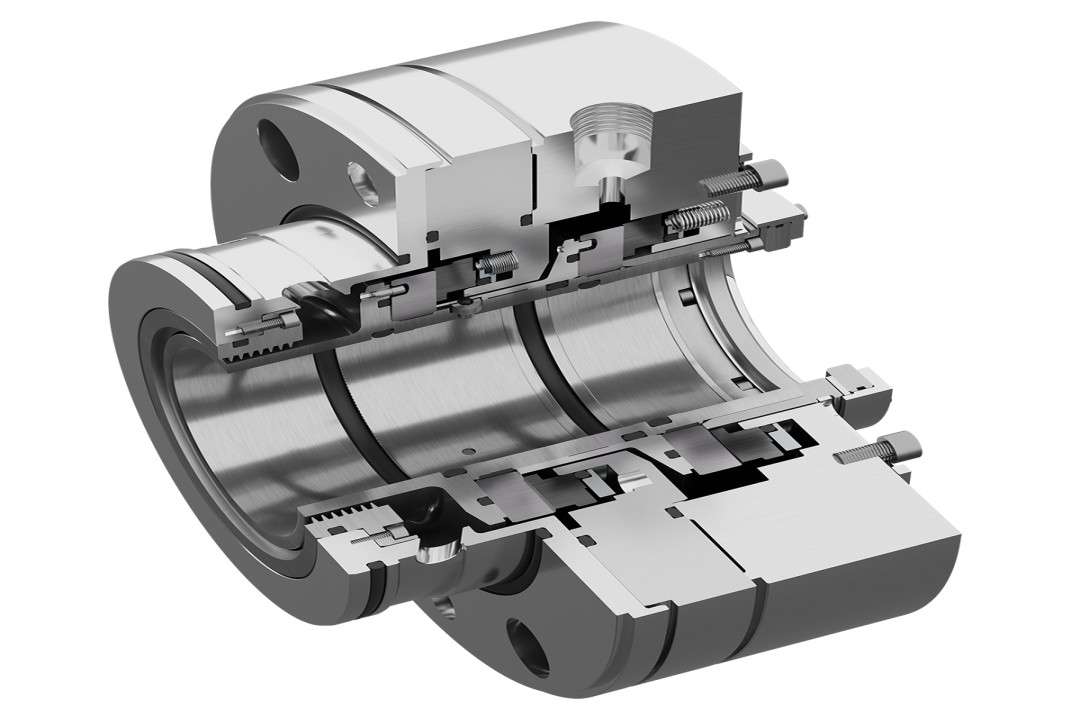
To address these challenges, John Crane engineered a retrofit solution that replaced the stuffing box with a mechanical seal system mounted at the rear of the pump. The design enabled installation without modifications to the existing pump structure and included a custom adapter sleeve to match the shaft configuration.
The sealing solution incorporates a controlled seal-flush system that maintains a clean fluid environment around the seal faces. Diamond-faced sealing materials were specified to provide durability and operational resilience in the event of pressure fluctuations or the ingress of solids into the seal chamber.
Following commissioning, the upgraded system has demonstrated strong operational performance. The seal-flush arrangement was designed for approximately 11 cubic metres of water per hour at 75 psi, while actual operating flow has averaged between 7.5 and 8 cubic metres per hour. By comparison, a parallel pump using traditional packing consumes approximately 20 cubic metres per hour.
This reduction of around 12 cubic metres per hour translates to an estimated saving of 288 cubic metres, or 288,000 litres, of water each day, depending on operating conditions at the site. The retrofit has also been designed to align maintenance activities with the mine’s annual planned service schedule, allowing seal maintenance to coincide with routine impeller and liner replacements and reducing the need for additional shutdowns.
According to Warren Smith, Global Mining Market Director at John Crane, the project demonstrates how advanced sealing technologies can enhance operational reliability, reduce maintenance requirements, and lower water consumption in demanding mining applications. The installation also marks a significant achievement for the company, featuring a shaft diameter of approximately 270 millimetres and representing the largest slurry seal supplied by John Crane to date.
John Crane is a worldwide provider of flow-control technologies and a pioneer in developing solutions for rotating equipment used across the energy and process sectors. Its offerings include mechanical seals, couplings, and filtration technologies, complemented by sophisticated service capabilities and digital monitoring tools. With a network of more than 200 service, sales, and manufacturing facilities in 50 countries, John Crane operates as a key business within Smiths Group plc, a FTSE 100 industrial technology leader committed to engineering progress for the future.