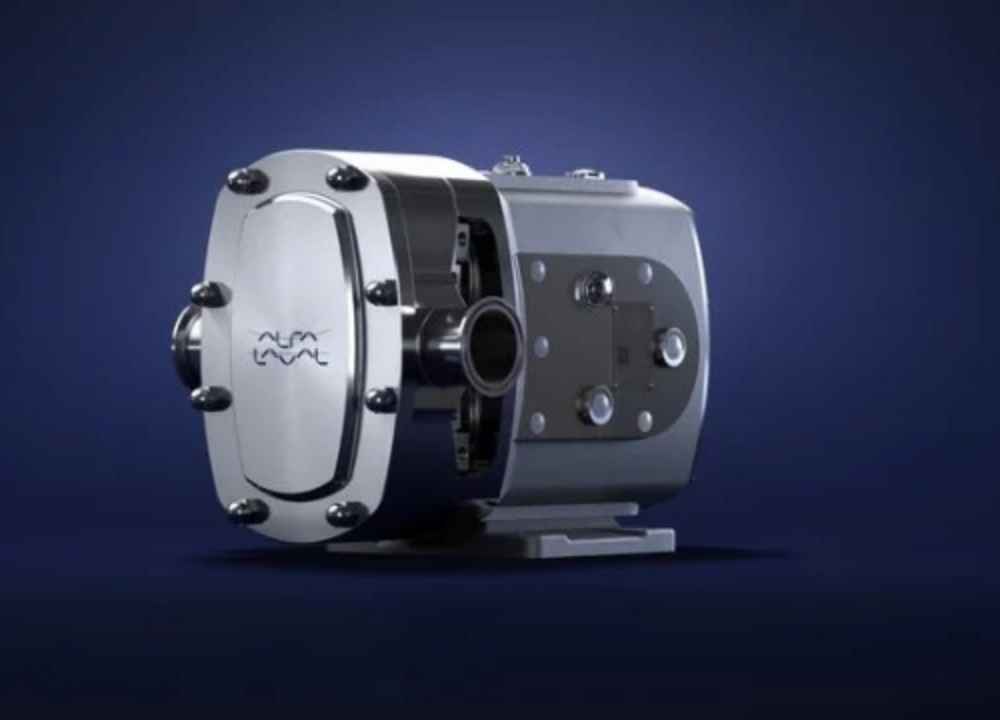
Alfa Laval has introduced its MaxiLobe and MaxiLobe UltraPure rotary lobe pump ranges for hygienic and high-purity processing. The positive displacement pumps are designed to improve volumetric efficiency, reduce energy consumption, simplify maintenance and increase equipment uptime, helping manufacturers lower the total cost of ownership.
The new pumps are intended for industries including dairy, food, beverages, home and personal care, pharmaceuticals and biotechnology. Their design supports a wider operating range and allows smaller pumps to handle specified duties at lower speeds in suitable applications.
Russ Kelly, Portfolio Manager, Pumps at Alfa Laval, said the new ranges build on the company’s experience in rotary lobe pumps. He said improved hygienic design and a wider operating range allow lower-speed operation, reducing shear and helping protect products that are sensitive to mechanical stress.
The pumps are designed to optimize capital expenditure through high volumetric efficiency and a broad flow and pressure range. Selecting a smaller pump for a particular application can reduce equipment and installation costs, including associated electrical equipment, while avoiding unnecessary oversizing.
The new ranges also simplify replacement of existing equipment. Their key porting dimensions match all Alfa Laval SRU pumps and most SX and SX UltraPure models, allowing upgrades without changes to existing pipework. Under specified operating conditions, MaxiLobe delivers at least 5% higher flow rates than the equivalent SRU model, potentially increasing process capacity without requiring additional installation space.
Lower operating speeds can reduce electricity consumption and operating costs. In many applications, the pumps can achieve energy savings of more than 25%. Reduced mechanical stress may also extend service intervals and equipment life. A robust gearbox design is intended to support reliable operation and reduce the risk of unplanned stoppages. Product quality and hygiene are supported by precision-profiled elastomers and cleanable designs. MaxiLobe pumps carry EHEDG and 3-A certification and comply with FDA requirements as standard.
MaxiLobe UltraPure is designed for pharmaceutical and biotechnology applications. It complies with ASME BPE standards and Good Manufacturing Practices guidelines, with material options and surface finishes suited to regulated manufacturing. Alfa Laval’s Q-doc documentation provides traceability and validation support, while material options meet relevant FDA and USP requirements.
Each pump is factory-tested and supplied with a performance certificate confirming compliance with its specified operating curve. Maintenance features include front-loading single seals that can be replaced without removing the pump from the process line. Interchangeable components and accessible shimming are intended to shorten service time. Alfa Laval’s global service organization provides additional maintenance support.
Alfa Laval provides solutions in heat transfer, separation and fluid handling for industries including energy, food, water, medicine, maritime transport and offshore operations. Founded more than 140 years ago, the company operates in over 100 countries and employs more than 23,500 people. Its 2025 annual sales were SEK 69.6 billion (€6.6 billion). Alfa Laval is listed on Nasdaq Stockholm.