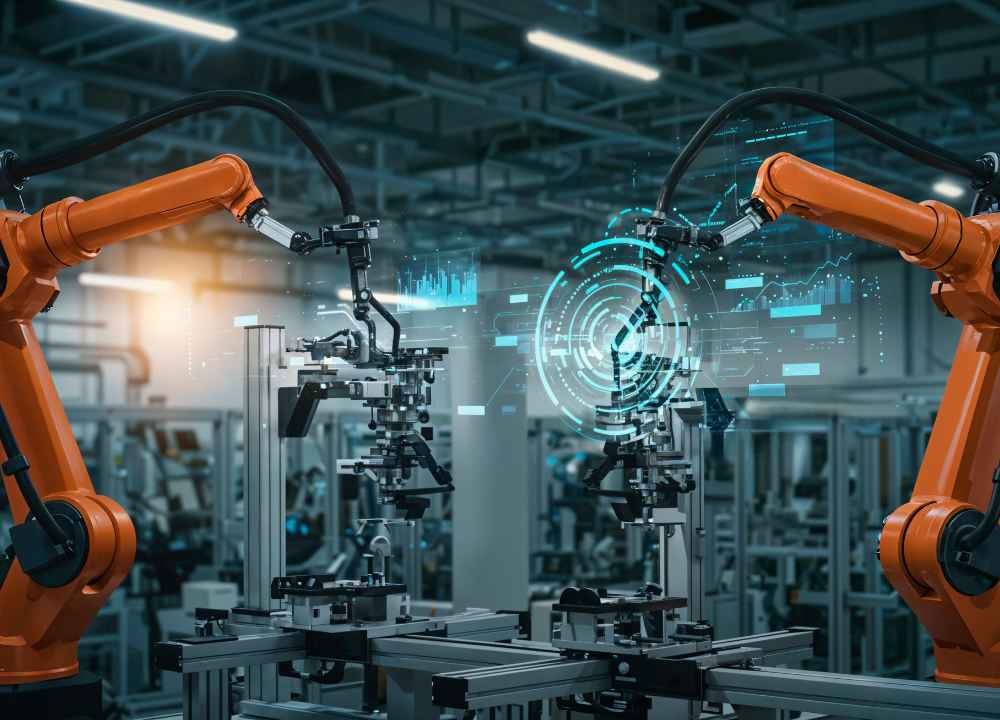
STMicroelectronics (NYSE: STM), a global leader in semiconductor technology, has launched a new family of 5MP CMOS image sensors: VD1943, VB1943, VD5943, and VB5943. These advanced ST BrightSense sensors are designed to support the rapid development of cutting-edge vision systems in sectors such as industrial automation, security, smart retail, and more. With applications ranging from enhanced machine and robotic vision to next-gen biometric identification and automated checkout, these sensors aim to revolutionize image capture across industries. Drawing on decades of expertise in optical sensing, ST is expanding its portfolio to meet the growing demand for high-performance, high-volume solutions.
The new sensors feature hybrid global and rolling shutter modes, providing unmatched flexibility for specific application needs. The global shutter ensures motion-artifact-free video capture, while the rolling shutter delivers low-noise, high-detail imaging. This combination is ideal for high-speed automated manufacturing, object tracking, and various other industrial applications.
Alexandre Balmefrezol, Executive Vice President and General Manager of STMicroelectronics’s Imaging Sub-Group, stated, “This unique architecture enables exceptional performance, making it a perfect solution for applications requiring both precision and high-speed imaging.”
These sensors use 2.25 µm pixel technology and advanced 3D stacking to deliver high image quality in a compact form factor. With a die size of 5.76 mm by 4.46 mm and a package size of just 10.3 mm by 8.9 mm, the sensors are designed for integration into space-constrained embedded vision systems. Their 73% pixel array-to-die surface ratio ensures optimal performance without sacrificing size. Additionally, the RGB-IR variants feature on-chip RGB-IR separation, simplifying system design and reducing component costs while maintaining full 5MP resolution for both color and infrared imaging. This integration enables flexible output patterns and independent exposure times, supporting a wide range of vision system designs.
The sensors are equipped with backside illumination (BSI) and capacitive deep trench isolation (CDTI) technologies, enhancing their performance in low-light conditions by increasing sensitivity and image sharpness. On-chip HDR (High Dynamic Range) further improves image quality, ensuring high visibility across both bright and dark areas. These advanced imaging features make the sensors ideal for high-demand applications such as machine vision and edge AI, where precise and reliable image capture is essential.
STMicroelectronics is a global semiconductor leader with over 50,000 employees, designing and producing a wide range of innovative products and solutions that help customers address challenges in industries ranging from automotive to industrial, consumer electronics, and energy management. With state-of-the-art manufacturing facilities and a commitment to sustainability, ST is on track to become carbon neutral by 2027. The company’s advanced technologies enable smarter mobility, energy-efficient systems, and the widespread adoption of connected autonomous devices, all while working toward a greener, more sustainable future.