Memsift Innovations has introduced three advanced membrane technology platforms aimed at transforming industrial water treatment, ultra-pure water production, and resource recovery applications across global industries. The newly launched platforms — NUCLEX™, HYPER-X-RO™, and MISTIL-PURE™ — are designed to address some of the most complex industrial wastewater and high-salinity treatment challenges while supporting the transition toward sustainable and circular manufacturing systems.
The launch marks a significant milestone for Memsift Innovations as industries worldwide continue to focus on water conservation, carbon reduction, waste minimization, and resource efficiency. The company stated that the three newly developed systems combine advanced membrane science, thermodynamic engineering, and modular process architecture to enable higher water recovery, improved operational stability, and enhanced resource extraction from industrial effluents. The technologies are intended for sectors including semiconductors, pharmaceuticals, chemicals, mining, energy, and advanced manufacturing, where industries increasingly require reliable, energy-efficient, and high-recovery water management solutions.
Dr J Antony Prince, Founder and CEO of Memsift Innovations, said the future of industrial sustainability will depend on how effectively industries manage water, energy, and waste as interconnected resources rather than isolated operational challenges. He noted that the newly launched platforms are the result of years of research and scientific innovation in membrane engineering, thermodynamics, and resource recovery systems.
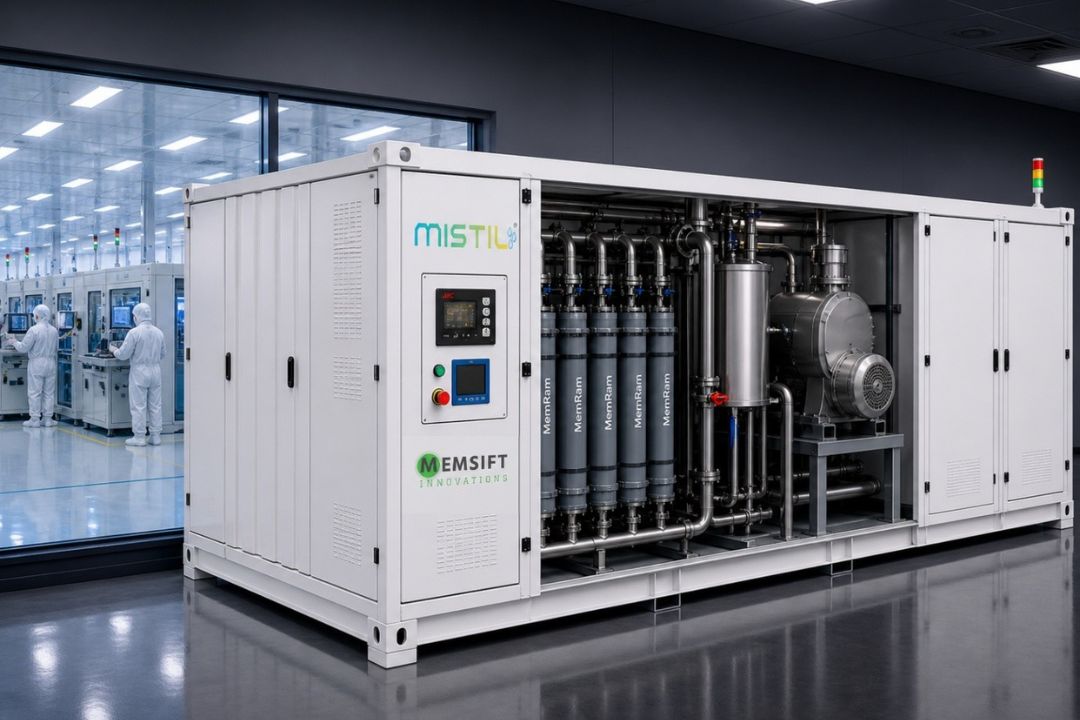
Among the three platforms, MISTIL-PURE™ has been developed as an advanced ultra-pure water production system based on improved membrane distillation technology. Designed primarily for semiconductor fabrication and AI-driven manufacturing facilities, the system operates using vapor-phase molecular separation, allowing only water vapor molecules to pass through specially engineered hydrophobic membranes while rejecting salts, metals, nanoparticles, silica, organics, endotoxins, and ionic contaminants with high efficiency.
According to the company, the system offers several operational advantages including improved contaminant rejection, stable ultra-pure water production under varying feed conditions, reduced chemical dependency, lower resin exhaustion, simplified polishing systems, and compatibility with low-grade heat recovery processes.
The second platform, HYPER-X-RO™, has been engineered to overcome conventional reverse osmosis limitations associated with extremely high salinity wastewater streams and industrial brines. Operating through a high-pressure batch recirculation process, the technology progressively concentrates dissolved salts and contaminants while continuously recovering purified water.
Memsift stated that HYPER-X-RO™ enables stable operation under ultra-high salinity conditions while achieving higher water recovery rates and lower specific energy consumption compared to conventional reverse osmosis systems. The platform also reduces residual brine volumes and improves integration with downstream crystallization systems.
The third platform, NUCLEX™, combines membrane distillation with controlled crystallization in a single integrated architecture for hypersaline wastewater treatment and resource recovery applications. Unlike traditional thermal crystallizers, the system uses vapor-phase separation to recover reusable water while simultaneously extracting high-purity salts and engineered crystalline products from industrial waste streams.
The company highlighted that NUCLEX™ can process ultra-high salinity brines beyond the operating limits of traditional reverse osmosis systems while reducing membrane scaling and fouling. Its compact modular architecture also allows seamless integration into Zero Liquid Discharge (ZLD) facilities.
Chris O’Connor, CFO and COO of Memsift Innovations, said the launch significantly strengthens the company’s position in the global industrial water treatment and resource recovery market. He added that the technologies are designed to work as a fully integrated platform covering pretreatment, concentration, ultra-pure water production, and resource extraction, enabling industries to improve recovery rates while lowering emissions and minimizing liquid waste.
Founded in 2018, Memsift Innovations focuses on developing advanced membrane technologies for sustainable industrial operations. The company’s portfolio includes membrane distillation, nanofiltration, ultrafiltration, high-salinity reverse osmosis, and membrane crystallization technologies designed to support circular manufacturing and energy-efficient industrial processes worldwide.