As manufacturing environments move towards higher precision, automation, and cleaner processes, the role of infrastructure is undergoing a quiet transformation. The shopfloor is no longer just a passive base; it is becoming an active enabler of safety, efficiency, and workflow optimisation. In this evolving space, Ecotile is redefining industrial flooring with modular, high-performance solutions designed for modern manufacturing facilities.
Ecotile, originally founded in 1996 in Hertfordshire, UK, has grown into a globally recognised manufacturer of industrial interlocking PVC flooring solutions, serving thousands of customers across manufacturing, aerospace, and commercial sectors worldwide. In India, the company operates through its local arm, headquartered in Mohali, Punjab, established in 2019 to meet the growing demand for high-performance industrial flooring solutions in the region. Over the years, Ecotile has built a strong reputation for durability, reliability, and innovation, with its UK-engineered products being adopted by leading global companies and critical industries where safety, uptime, and long-term performance are essential.
At the upcoming AeroDef India Manufacturing Expo 2026, Ecotile is set to showcase how flooring can directly influence productivity and operational continuity. In an exclusive interaction with Machine Maker, Tushar Dhawan shares how the company is enabling industries to rethink their shopfloor infrastructure, especially in sectors where downtime and contamination risks cannot be afforded.
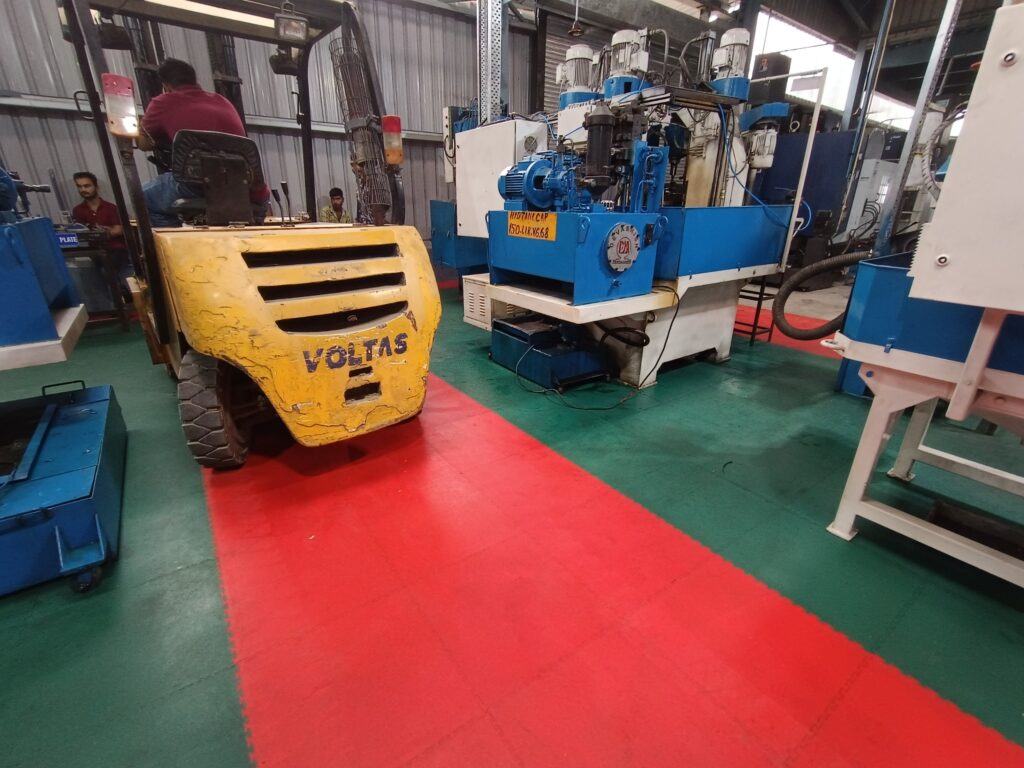
Designed for Zero Downtime and High-Performance Shopfloors
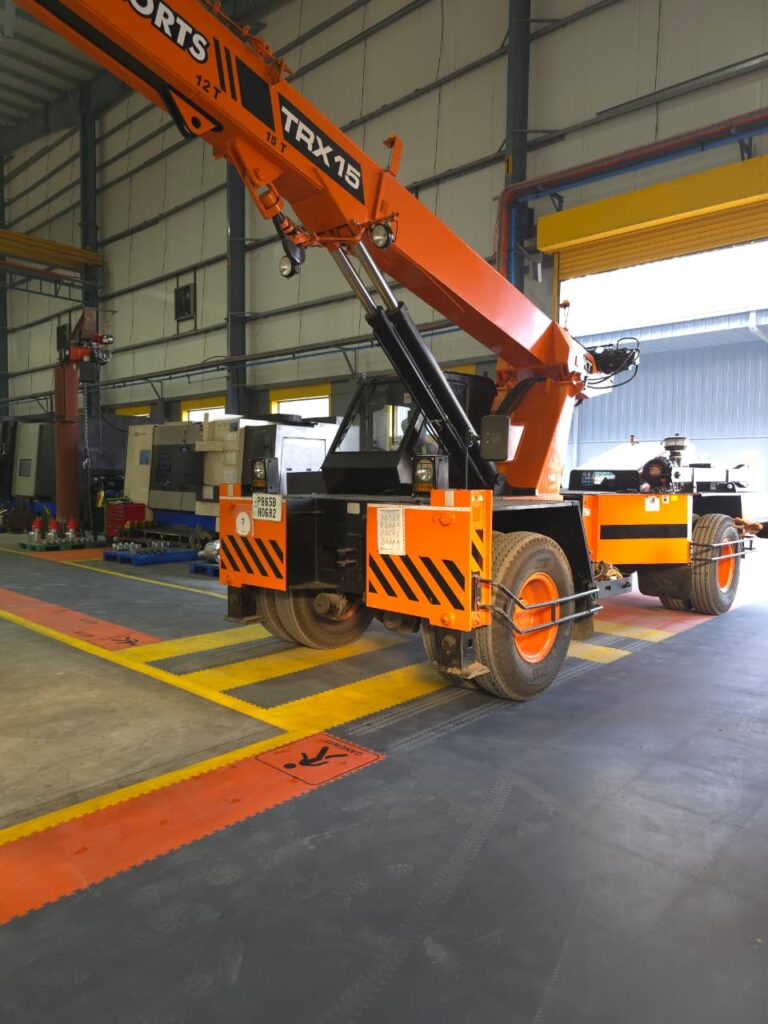
“Ecotile’s core offering lies in its interlocking modular PVC tile system, engineered to perform in demanding industrial environments. Designed in the UK, these flooring systems are built to handle heavy loads, forklift traffic, and chemical exposure while maintaining long-term durability and stability”, said Tushar Dhawan.
What differentiates Ecotile is its ability to eliminate one of the biggest pain points in manufacturing downtime during installation. Unlike traditional epoxy or coated flooring systems that require shutdowns and curing time, Ecotile’s adhesive-free interlocking design allows installation to happen alongside ongoing operations. This becomes especially critical in aerospace, defence, and electronics environments, where production continuity is directly linked to business performance.
“The modular nature of the system also allows individual tiles to be replaced without disrupting the entire floor, making maintenance faster and more cost-efficient”, adds Mr Dhawan.
Beyond durability, Ecotile is also addressing evolving industry requirements, including ESD (electrostatic discharge) control, cleanroom compatibility, and enhanced safety through anti-slip surfaces. Their specialised flooring solutions are designed to support sensitive environments, including electronics manufacturing and defence applications, where static control and contamination management are essential. Another dimension of Ecotile’s offering lies in shopfloor organisation and visual management.
“With options for colour-coded zones, walkways, and safety demarcations, the flooring system contributes to lean manufacturing practices, helping industries improve workflow clarity and workforce safety”, shares Tushar Dhawan.
Ecotile’s Growing Footprint Across Leading Industries
Over the years, Ecotile has built a strong, credible clientele across industries by consistently delivering flooring solutions that address real operational challenges. Its adoption by leading organisations such as Jindal Stainless, Maruti Suzuki, Hindalco Industries, Mahindra & Mahindra, Indian Navy, Hindustan Aeronautics Limited, Tata Advanced Systems, Tata Motors, and Reliance Industries reflects the company’s ability to meet the stringent requirements of high-performance industrial environments. This diverse customer base spanning automotive, metals, aerospace, defence, and large-scale manufacturing demonstrates how Ecotile has positioned itself as a reliable infrastructure partner for mission-critical operations.
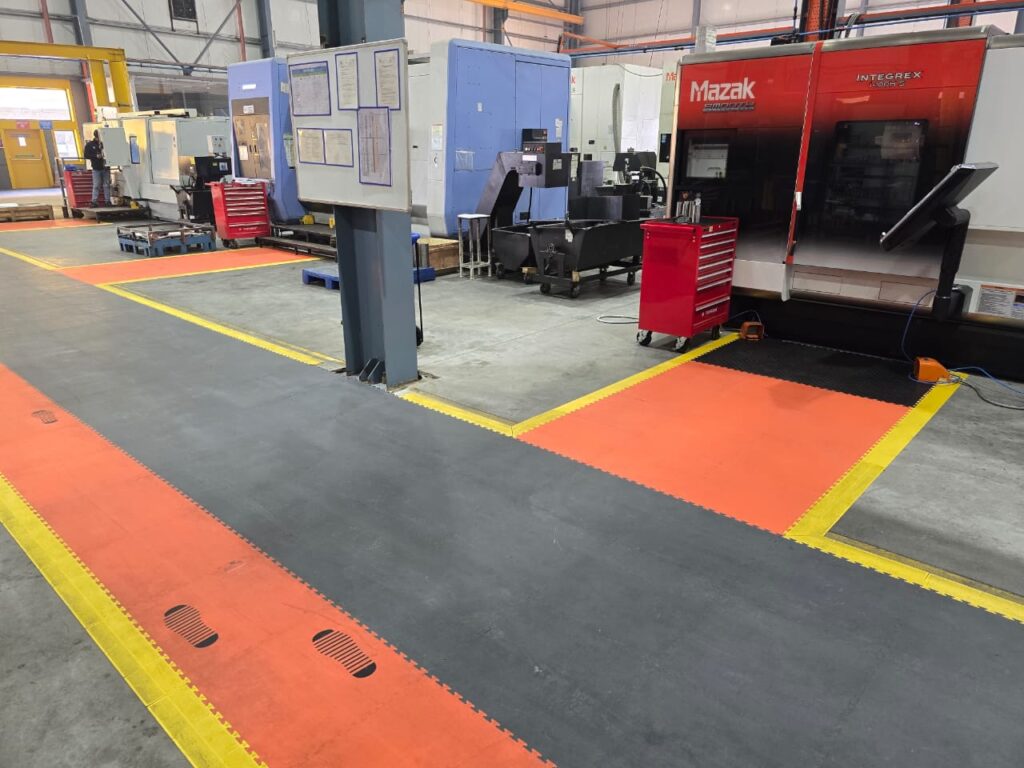
The applications of Ecotile flooring span a wide spectrum of industrial and commercial environments, from manufacturing facilities and warehousing to electronics production, aerospace, and defence. The system is engineered to support heavy-duty usage, including forklift traffic, pallet movement, and high-load operations, while also catering to specialised needs such as cleanrooms, ESD-controlled environments, and safety-marked shopfloors.
Its modular design allows seamless installation over uneven or damaged surfaces, making it particularly suitable for retrofit projects where maintaining continuity is essential. As highlighted in the company’s brochure, Ecotile solutions are already being deployed across industries such as automotive, warehousing, aerospace, and defence, reinforcing its role in enabling safer, more efficient, and visually organised shopfloors.
Sustainability is also built into the system. “Ecotile tiles are designed to be long-lasting and recyclable, aligning with the growing focus on environmentally responsible manufacturing practices”, shared Tushar Dhawan. As industries increasingly recognise that productivity is influenced not just by machines but by the environment in which they operate, Ecotile’s presence at AeroDef highlights an important shift. The conversation in manufacturing is expanding from equipment and components to the ecosystem that supports precision production.