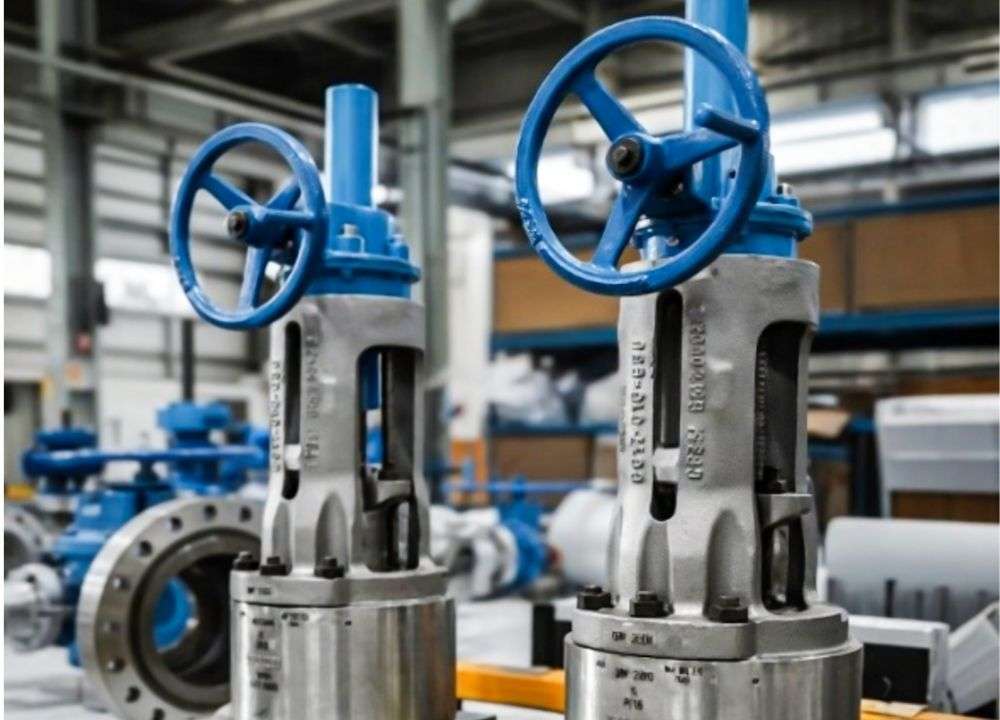
Velan has supplied a package of severe-service valves for a major residue-upgrading project at an Indian refinery completed in 2026. The equipment is designed for an ebullated-bed residue hydrocracking unit that converts heavy fractions of crude oil into higher-value products, including naphtha, gasoline and vacuum gas oil.
The unit processes vacuum resid, the heaviest fraction of crude oil, under demanding operating conditions. The process operates at approximately 454°C and 196 kg/cm², equivalent to around 2,788 psi. These conditions expose valves and flow-control equipment to high temperatures, pressure and solids-laden media, increasing the risk of erosion, fouling and coke accumulation.
Velan’s supply package includes Securaseal R-Series metal-seated ball valves, chopper valves, control valves, motor-operated and automated on/off valves, manual valves and purge-line configurations. The package also includes four high-pressure control valves and several fast-acting chopper valves certified to Safety Integrity Level (SIL) requirements.
The R-Series valves incorporate Velan’s Hexa-Shield thermal protection and Securaring pressure-energised sealing technology. These features are intended to support sealing performance and reliability under demanding temperature and pressure conditions. The equipment has been installed across different sections of the unit to support isolation, process switching, flow control and staged pressure reduction. Severe-service ball valves are also installed on two pressure-letdown skids designed and manufactured in India by a local skid manufacturer under a partnership agreement.
Velan supplied purge panels to regulate purge-fluid flow through critical lines. The purge arrangements are intended to help keep valve areas clear of coke deposits, protecting equipment and supporting reliable operation. Hexa-Shield uses a double-walled thermal protection design suited to high-cycle catalyst-handling service. The Securaring system uses pressure-energised sealing to help maintain sealing stability under severe operating conditions. Together with the purge-line arrangements, these technologies address challenges associated with residue hydrocracking processes.
According to Velan, the valve selection followed approval by the project licensor and was based on the technical requirements of the application and the company’s experience in severe-service operations. The project involved coordination between Velan’s North American and Indian teams, with manufacturing in India supporting local execution. The company said the work demonstrates its ability to provide specialised valve solutions for refinery applications involving high pressure, high temperature and abrasive process media.
The refinery project is also significant because it represents the first application of this slurry hydrocracking technology in India. The installation provides a reference for Velan in a specialised process area where equipment reliability is essential to maintaining safe and continuous operations.
Velan’s supply covers several functions within the unit, from process control and isolation to pressure reduction and equipment protection. The package is designed to support the operating requirements of the residue-upgrading process while managing the risks associated with coke formation and demanding service conditions.