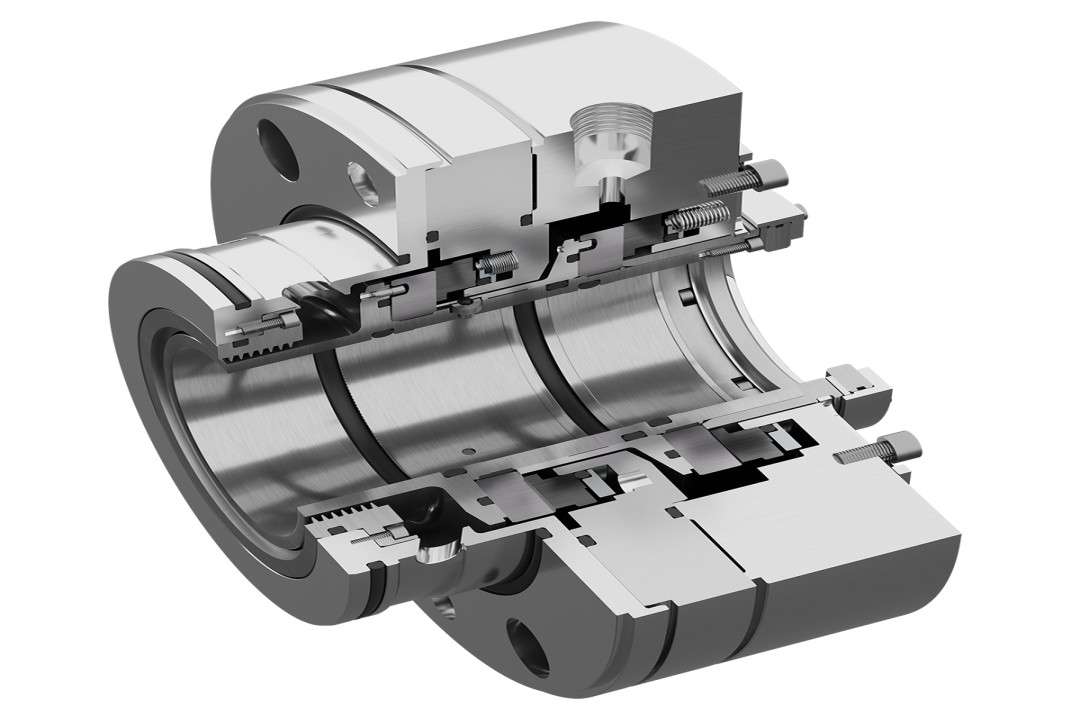
John Crane, a global provider of flow control technologies and a business of Smiths Group plc, has been honoured with the Most Innovative Water Management Solution award at the Manufacturing Supplier Innovation Awards UK 2026 for its Type SB2 USP technology. The recognition highlights the company’s contribution to developing advanced solutions that help industries reduce water consumption while maintaining high standards of operational performance and equipment reliability.
The Manufacturing Supplier Innovation Awards celebrate companies that introduce technologies capable of addressing major industrial challenges through innovation. John Crane received the award for a sealing solution that enables industrial facilities to significantly lower water usage without affecting safety, efficiency or equipment performance.
The Type SB2 USP technology has been developed to support customers operating in demanding industrial environments where water conservation and operational reliability are equally important. By improving sealing efficiency, the technology minimises water consumption while ensuring continuous performance in critical applications across the energy and process industries.
One of the most notable deployments of the technology was at a liquefied natural gas (LNG) facility, where it helped reduce water consumption from nearly 2,000 gallons per day to only 3–4 gallons per day. The dramatic reduction demonstrates the technology’s ability to conserve natural resources while maintaining the integrity and reliability of industrial equipment operating under challenging conditions.
Mike Eason, Chief Technology Officer at John Crane, said the award reflects the dedication and technical expertise of the company’s global engineering teams. He noted that industries worldwide are under increasing pressure to improve sustainability while maintaining operational efficiency and reliability. According to him, technologies such as the Type SB2 USP enable customers to meet both objectives by reducing resource consumption without compromising performance.
John Crane has continued to invest in research and product development focused on helping industrial customers improve operational efficiency, reduce environmental impact and support long-term sustainability goals. The latest recognition reinforces the company’s efforts to deliver practical technologies that address evolving customer requirements across sectors including energy, petrochemicals, refining and industrial processing.
The award also acknowledges the growing importance of water management in industrial operations as companies seek to optimise resource utilisation, lower operating costs and comply with increasingly stringent environmental standards. Advanced sealing technologies play a vital role in achieving these objectives by reducing waste and improving overall system efficiency.
Libbie Hammond, Editor of Manufacturing Today magazine, congratulated John Crane on the achievement, stating that the company had demonstrated how innovation within the manufacturing supply chain can deliver measurable environmental and operational benefits. She noted that the awards continue to showcase suppliers that are making a meaningful contribution to industrial progress through practical, high-impact technologies.
The recognition further strengthens John Crane’s position as a technology leader committed to supporting customers with solutions that enhance equipment performance while promoting responsible resource management. As industries continue to pursue sustainable manufacturing practices, innovations such as the Type SB2 USP are expected to play an increasingly important role in helping organisations reduce water usage, improve efficiency and build more resilient operations.