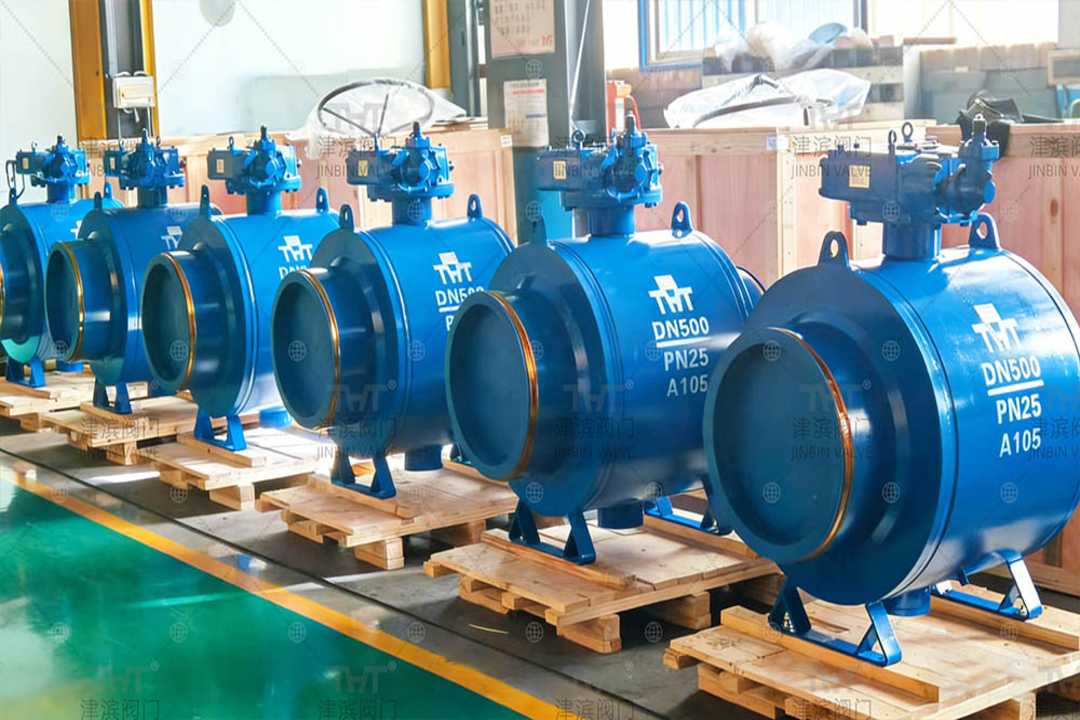
JINBIN Valves has announced the successful completion and testing of a custom-built DN600 bidirectional soft-sealed knife gate valve, developed to meet the requirements of large-scale industrial pipeline systems. The product has undergone rigorous testing and factory inspection, with all performance parameters meeting established industry benchmarks.
Engineered for demanding operating environments, the DN600 knife gate valve is designed to support efficient flow control and medium isolation across a range of sectors, including wastewater treatment, chemical processing, metallurgy, power generation, municipal water systems, and mining operations. Its design ensures reliable performance in conditions requiring high sealing efficiency and resistance to pressure variations.
The valve is constructed using high-grade ductile iron, providing durability and structural stability. Advanced CNC machining techniques have been applied to achieve precise dimensions and consistent product quality. The sealing system incorporates premium PTFE soft materials, enabling effective sealing and ensuring zero leakage under standard operating conditions.
Performance validation included a series of functional and pressure tests. The valve demonstrated smooth and responsive operation, while pressure testing confirmed strong sealing integrity and consistent performance. The product is suitable for DN600 pipeline systems and supports pressure ratings ranging from PN10 to PN16. It is designed to operate within a temperature range of -20°C to 200°C, making it adaptable to a wide variety of industrial processes.
The development of this customised solution highlights JINBIN Valves’ focus on addressing specific client requirements through tailored engineering and manufacturing capabilities. By combining material quality, precision manufacturing, and thorough testing protocols, the company continues to deliver solutions aligned with the operational demands of modern industry.
JINBIN Valves stated that the successful delivery of the DN600 knife gate valve reinforces its commitment to quality, reliability, and innovation in valve manufacturing. The company continues to expand its product portfolio to meet the evolving needs of industrial customers across global markets.
With increasing demand for robust and efficient flow control systems, JINBIN Valves remains focused on enhancing its production capabilities and supporting clients with dependable, high-performance products. The company aims to strengthen its presence in key industrial sectors by delivering solutions that ensure operational efficiency, safety, and long-term reliability.