Electrochemical machining (ECM) enables high-precision deburring and
rounding of workpiece edges using electrolysis. Pre- or post-cleaning
ensures the stable functioning of the process and ensures that the surface
finish meets defined cleanliness specifications. A manufacturer of ECM
solutions therefore integrates ultrasonic cleaning modules into its
individually manufactured systems.
Founded in 2007, VULIC ECM GmbH & Co KG initially focused on the
development and manufacture of customer-specific devices (tools) and spare
parts for electrochemical metal machining (ECM). Seven years later, the
first ECM system developed in-house followed with the V 500 machining
center and the established service portfolio was expanded to include
contract machining. The modularly designed standard and special systems and
services of the Ottobeuren-based company are now in demand internationally
from customers in the automotive, defense, aerospace and medical technology
industries, among others.
Integrated ultrasonic cleaning for stable ECM processes and high cleanliness
In ECM technology, burrs can be efficiently removed and edges rounded with
high precision, even in hard-to-reach areas such as blind holes, bore
intersections and pockets. For the non-contact process, the tool is
connected to a direct current source as the cathode (negative) and the
component is polarized as the anode (positive). The charge exchange takes
place in a saline electrolyte solution, whereby the burrs are completely
dissolved and removed from the working gap by the electrolyte. “For the
quality and precision of ECM processes, it is crucial that the parts to be
machined are free of oil and grease,” explains Sascha Haushammer, Sales
Manager at VULIC ECM. “In addition, enormously increased cleanliness
requirements usually require cleaning after the ECM process to remove
electrolyte residues and any particles adhering to the component.” For
these reasons, the system manufacturer has also been offering its machines
with integrated modules for pre- and post-cleaning, for example with
ultrasonic, since 2018 and also uses them in the service sector. VULIC ECM
manufactures the cleaning tanks in-house to customer specifications, now
also for applications without ECM. The company was looking for an efficient
partner for the ultrasonic equipment.
One company for cleaning media recommended Weber Ultrasonics AG. The
internationally active company develops and produces ultrasonic components
for cleaning, welding and cutting. The generators for component cleaning
are available in different frequencies, also as multi-frequency systems. In
combination with frequency-adapted plate, immersion and rod transducers,
they enable the construction of compact cleaning solutions that are
individually tailored to the workpieces and cleanliness requirements. “We
also spoke to other manufacturers at the time, but the collaboration with
Weber Ultrasonics worked so well right from the start that we didn’t bring
any other suppliers on board,” reports Sascha Haushammer. “We receive very
good advice and have been able to build up a certain amount of expertise in
ultrasonic cleaning over the years. Today, we only really need the
expertise of Weber Ultrasonics for special projects.”
Edge rounding and cleaning of kilometer-long metal strips
One such project was the development and production of a complete solution
for processing steel strips of different widths and thicknesses and several
kilometers in length. The task actually sounded simple: to produce a
defined edge rounding on one side of the parts and prepare them for
subsequent preservation by the customer. “The process speed was also an
important factor,” explains Sascha Haushammer. VULIC ECM designed a modular
throughfeed system with pre-cleaning, ECM processing and post-cleaning
stations including ultrasonic.
The module for post-cleaning consists of three separate zones. The middle
zone is equipped with a 25 kHz Sonosub transducer with 500 watts of power
on the floor side. The laser-welded capsule of the transducer is extremely
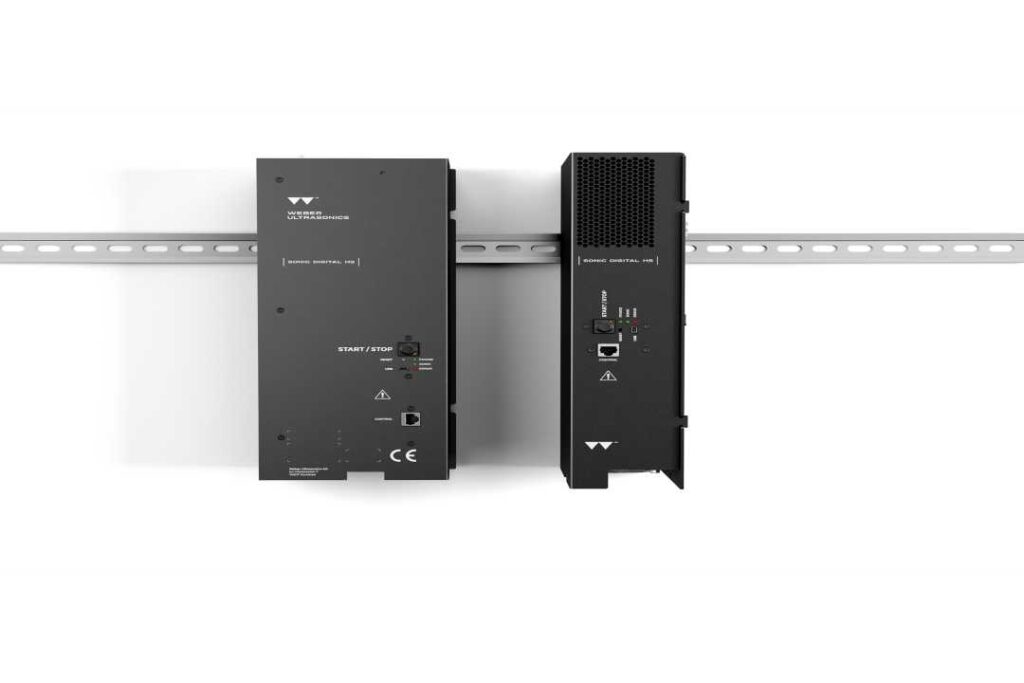
smooth and therefore minimizes deposits. With the Sonic Digital HS3
generator, which has been adapted in terms of output, the frequency of 25
kHz is digitally generated, controlled and monitored by a 32-bit
microcontroller. The power can be regulated in the range from 10 to 100
percent in 1% increments, which allows optimum adaptation to part-specific
cleaning programs.
Processing and cleaning at high process speeds
The belts, which are slightly contaminated with oil, are unwound on the
infeed side using a decoiler and undergo a combined spray and brush pre-
cleaning in the first station. Edge rounding takes place in the middle
module. At the post-cleaning station, the steel strip is sprayed off in the
first zone and completely drawn into the tank filled with cleaning medium
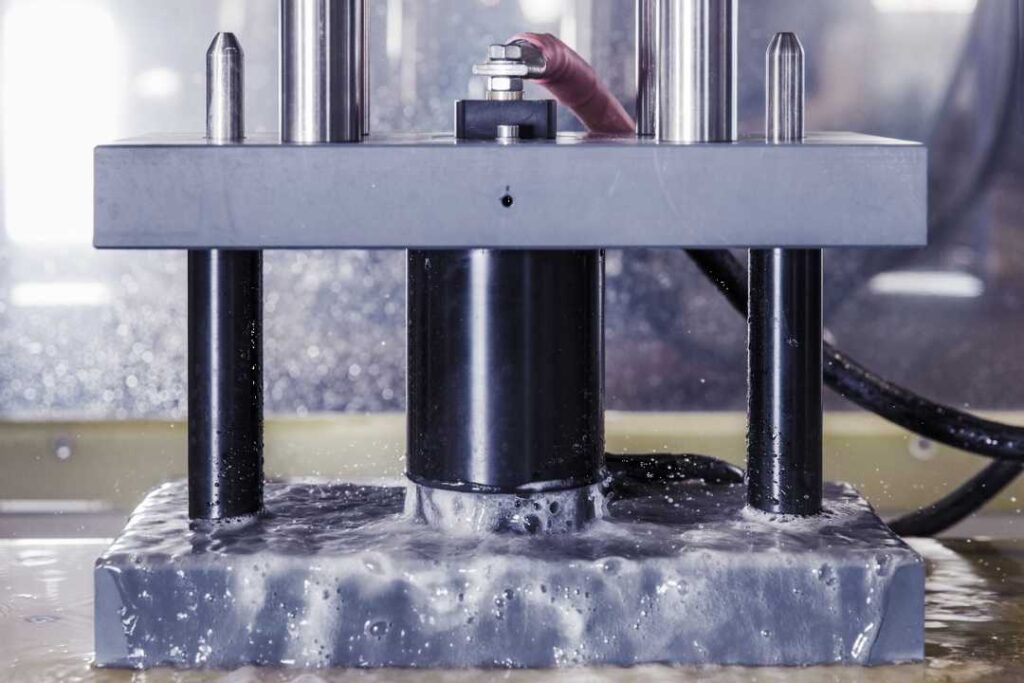
via a roller in zone 2. In this liquid bath, the ultrasound develops its
effect through acoustic cavitation: the immersible transducer transmits the
electrical signals generated by the generator into the liquid, creating an
alternation of negative and positive pressure. In the negative pressure
phases, microscopically small cavities are formed, which collapse (implode)
in the subsequent positive pressure phase. This creates shock waves with
considerable energy, which “blast off” particulate and filmic-chemical
contamination. At the same time, microflows develop which flush away
detached or dissolved contaminants. The belts are transported via another
roller to zone 3, which is equipped with a hot-air drying system. They are
then protected against corrosion in the customer’s preservation unit before
being rolled up again. Integrated post-cleaning with ultrasonic
Inline Cleaning After EMC Deburring – For Residue-Free Strip Surfaces
Electrochemical machining (ECM) enables high-precision deburring and
rounding of workpiece edges using electrolysis. Pre- or post-cleaning
ensures the stable functioning of the process and ensures that the surface
finish meets defined cleanliness specifications. A manufacturer of ECM
solutions therefore integrates ultrasonic cleaning modules into its
individually manufactured systems.
Founded in 2007, VULIC ECM GmbH & Co. KG initially focused on the
development and manufacture of customer-specific devices (tools) and spare
parts for electrochemical metal machining (ECM). Seven years later, the
first ECM system developed in-house followed with the V 500 machining
center and the established service portfolio was expanded to include
contract machining. The modularly designed standard and special systems and
services of the Ottobeuren-based company are now in demand internationally
from customers in the automotive, defense, aerospace and medical technology
industries, among others.
Integrated ultrasonic cleaning for stable ECM processes and high cleanliness
In ECM technology, burrs can be efficiently removed and edges rounded with
high precision, even in hard-to-reach areas such as blind holes, bore
intersections and pockets. For the non-contact process, the tool is
connected to a direct current source as the cathode (negative) and the
component is polarized as the anode (positive). The charge exchange takes
place in a saline electrolyte solution, whereby the burrs are completely
dissolved and removed from the working gap by the electrolyte. “For the
quality and precision of ECM processes, it is crucial that the parts to be
machined are free of oil and grease,” explains Sascha Haushammer, Sales
Manager at VULIC ECM. “In addition, enormously increased cleanliness
requirements usually require cleaning after the ECM process to remove
electrolyte residues and any particles adhering to the component.” For
these reasons, the system manufacturer has also been offering its machines
with integrated modules for pre- and post-cleaning, for example with
ultrasonic, since 2018 and also uses them in the service sector. VULIC ECM
manufactures the cleaning tanks in-house to customer specifications, now
also for applications without ECM. The company was looking for an efficient
partner for the ultrasonic equipment.
Ultrasonic adapted to the respective application
One company for cleaning media recommended Weber Ultrasonics AG. The
internationally active company develops and produces ultrasonic components
for cleaning, welding and cutting. The generators for component cleaning
are available in different frequencies, also as multi-frequency systems. In
combination with frequency-adapted plate, immersion and rod transducers,
they enable the construction of compact cleaning solutions that are
individually tailored to the workpieces and cleanliness requirements. “We
also spoke to other manufacturers at the time, but the collaboration with
Weber Ultrasonics worked so well right from the start that we didn’t bring
any other suppliers on board,” reports Sascha Haushammer. “We receive very
good advice and have been able to build up a certain amount of expertise in
ultrasonic cleaning over the years. Today, we only really need the
expertise of Weber Ultrasonics for special projects.”
Edge rounding and cleaning of kilometer-long metal strips
One such project was the development and production of a complete solution
for processing steel strips of different widths and thicknesses and several
kilometers in length. The task actually sounded simple: to produce a
defined edge rounding on one side of the parts and prepare them for
subsequent preservation by the customer. “The process speed was also an
important factor,” explains Sascha Haushammer. VULIC ECM designed a modular
throughfeed system with pre-cleaning, ECM processing and post-cleaning
stations including ultrasonic.
The module for post-cleaning consists of three separate zones. The middle
zone is equipped with a 25 kHz Sonosub transducer with 500 watts of power
on the floor side. The laser-welded capsule of the transducer is extremely
smooth and therefore minimizes deposits. With the Sonic Digital HS3
generator, which has been adapted in terms of output, the frequency of 25
kHz is digitally generated, controlled and monitored by a 32-bit
microcontroller. The power can be regulated in the range from 10 to 100
percent in 1% increments, which allows optimum adaptation to part-specific
cleaning programs.
Processing and cleaning at high process speeds
The belts, which are slightly contaminated with oil, are unwound on the
infeed side using a decoiler and undergo a combined spray and brush pre-
cleaning in the first station. Edge rounding takes place in the middle
module. At the post-cleaning station, the steel strip is sprayed off in the
first zone and completely drawn into the tank filled with cleaning medium
via a roller in zone 2. In this liquid bath, the ultrasound develops its
effect through acoustic cavitation: the immersible transducer transmits the
electrical signals generated by the generator into the liquid, creating an
alternation of negative and positive pressure. In the negative pressure
phases, microscopically small cavities are formed, which collapse (implode)
in the subsequent positive pressure phase. This creates shock waves with
considerable energy, which “blast off” particulate and filmic-chemical
contamination. At the same time, microflows develop which flush away
detached or dissolved contaminants. The belts are transported via another
roller to zone 3, which is equipped with a hot-air drying system. They are
then protected against corrosion in the customer’s preservation unit before
being rolled up again. Integrated post-cleaning with ultrasonic
Inline Cleaning After EMC Deburring – For Residue-Free Strip Surfaces
Electrochemical machining (ECM) enables high-precision deburring and
rounding of workpiece edges using electrolysis. Pre- or post-cleaning
ensures the stable functioning of the process and ensures that the surface
finish meets defined cleanliness specifications. A manufacturer of ECM
solutions therefore integrates ultrasonic cleaning modules into its
individually manufactured systems.
Founded in 2007, VULIC ECM GmbH & Co. KG initially focused on the
development and manufacture of customer-specific devices (tools) and spare
parts for electrochemical metal machining (ECM). Seven years later, the
first ECM system developed in-house followed with the V 500 machining
center and the established service portfolio was expanded to include
contract machining. The modularly designed standard and special systems and
services of the Ottobeuren-based company are now in demand internationally
from customers in the automotive, defense, aerospace and medical technology
industries, among others.
Integrated ultrasonic cleaning for stable ECM processes and high cleanliness
In ECM technology, burrs can be efficiently removed and edges rounded with
high precision, even in hard-to-reach areas such as blind holes, bore
intersections and pockets. For the non-contact process, the tool is
connected to a direct current source as the cathode (negative) and the
component is polarized as the anode (positive). The charge exchange takes
place in a saline electrolyte solution, whereby the burrs are completely
dissolved and removed from the working gap by the electrolyte. “For the
quality and precision of ECM processes, it is crucial that the parts to be
machined are free of oil and grease,” explains Sascha Haushammer, Sales
Manager at VULIC ECM. “In addition, enormously increased cleanliness
requirements usually require cleaning after the ECM process to remove
electrolyte residues and any particles adhering to the component.” For
these reasons, the system manufacturer has also been offering its machines
with integrated modules for pre- and post-cleaning, for example with
ultrasonic, since 2018 and also uses them in the service sector. VULIC ECM
manufactures the cleaning tanks in-house to customer specifications, now
also for applications without ECM. The company was looking for an efficient
partner for the ultrasonic equipment.
One company for cleaning media recommended Weber Ultrasonics AG. The
internationally active company develops and produces ultrasonic components
for cleaning, welding and cutting. The generators for component cleaning
are available in different frequencies, also as multi-frequency systems. In
combination with frequency-adapted plate, immersion and rod transducers,
they enable the construction of compact cleaning solutions that are
individually tailored to the workpieces and cleanliness requirements. “We
also spoke to other manufacturers at the time, but the collaboration with
Weber Ultrasonics worked so well right from the start that we didn’t bring
any other suppliers on board,” reports Sascha Haushammer. “We receive very
good advice and have been able to build up a certain amount of expertise in
ultrasonic cleaning over the years. Today, we only really need the
expertise of Weber Ultrasonics for special projects.”
Ultrasonic adapted to the respective application
One company for cleaning media recommended Weber Ultrasonics AG. The
internationally active company develops and produces ultrasonic components
for cleaning, welding and cutting. The generators for component cleaning
are available in different frequencies, also as multi-frequency systems. In
combination with frequency-adapted plate, immersion and rod transducers,
they enable the construction of compact cleaning solutions that are
individually tailored to the workpieces and cleanliness requirements. “We
also spoke to other manufacturers at the time, but the collaboration with
Weber Ultrasonics worked so well right from the start that we didn’t bring
any other suppliers on board,” reports Sascha Haushammer. “We receive very
good advice and have been able to build up a certain amount of expertise in
ultrasonic cleaning over the years. Today, we only really need the
expertise of Weber Ultrasonics for special projects.”
Edge rounding and cleaning of kilometer-long metal strips
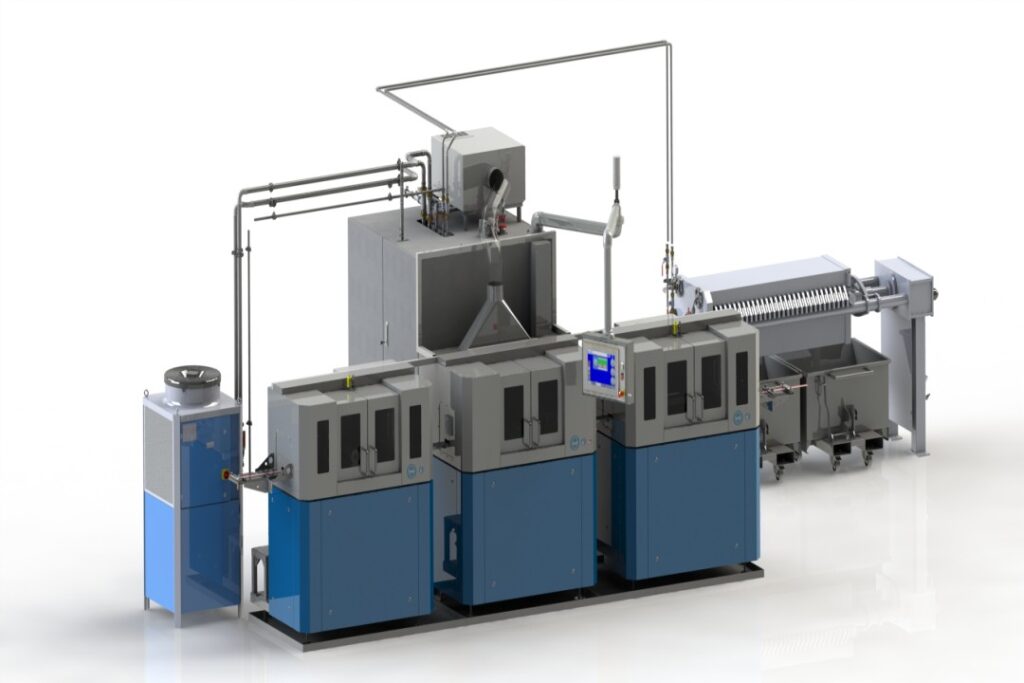
One such project was the development and production of a complete solution
for processing steel strips of different widths and thicknesses and several
kilometers in length. The task actually sounded simple: to produce a
defined edge rounding on one side of the parts and prepare them for
subsequent preservation by the customer. “The process speed was also an
important factor,” explains Sascha Haushammer. VULIC ECM designed a modular
throughfeed system with pre-cleaning, ECM processing and post-cleaning
stations including ultrasonic.
The module for post-cleaning consists of three separate zones. The middle
zone is equipped with a 25 kHz Sonosub transducer with 500 watts of power
on the floor side. The laser-welded capsule of the transducer is extremely
smooth and therefore minimizes deposits. With the Sonic Digital HS3
generator, which has been adapted in terms of output, the frequency of 25
kHz is digitally generated, controlled and monitored by a 32-bit
microcontroller. The power can be regulated in the range from 10 to 100
percent in 1% increments, which allows optimum adaptation to part-specific
cleaning programs.
Processing and cleaning at high process speeds
The belts, which are slightly contaminated with oil, are unwound on the
infeed side using a decoiler and undergo a combined spray and brush pre-
cleaning in the first station. Edge rounding takes place in the middle
module. At the post-cleaning station, the steel strip is sprayed off in the
first zone and completely drawn into the tank filled with cleaning medium
via a roller in zone 2. In this liquid bath, the ultrasound develops its
effect through acoustic cavitation: the immersible transducer transmits the
electrical signals generated by the generator into the liquid, creating an
alternation of negative and positive pressure. In the negative pressure
phases, microscopically small cavities are formed, which collapse (implode)
in the subsequent positive pressure phase. This creates shock waves with
considerable energy, which “blast off” particulate and filmic-chemical
contamination. At the same time, microflows develop which flush away
detached or dissolved contaminants. The belts are transported via another
roller to zone 3, which is equipped with a hot-air drying system. They are
then protected against corrosion in the customer’s preservation unit before
being rolled up again.